Technology16 September 2026
Stick packs vs sachets: choosing the right single-serve format
Both single-serve formats form, fill, seal and cut single-dose packs from film at high speed. But choosing between them should start with production needs, not appearance.
How each pack is formed changes what it can hold, how much film it uses, how it behaves through cartoning, and how the customer opens it. This guide sets out where the two formats differ in practice and what should be settled before a machine is specified.
How each pack is formed
Both options are vertical form fill seal processes running off reel film, and both are multi-lane. What differs is how the film is folded and where the seals land.
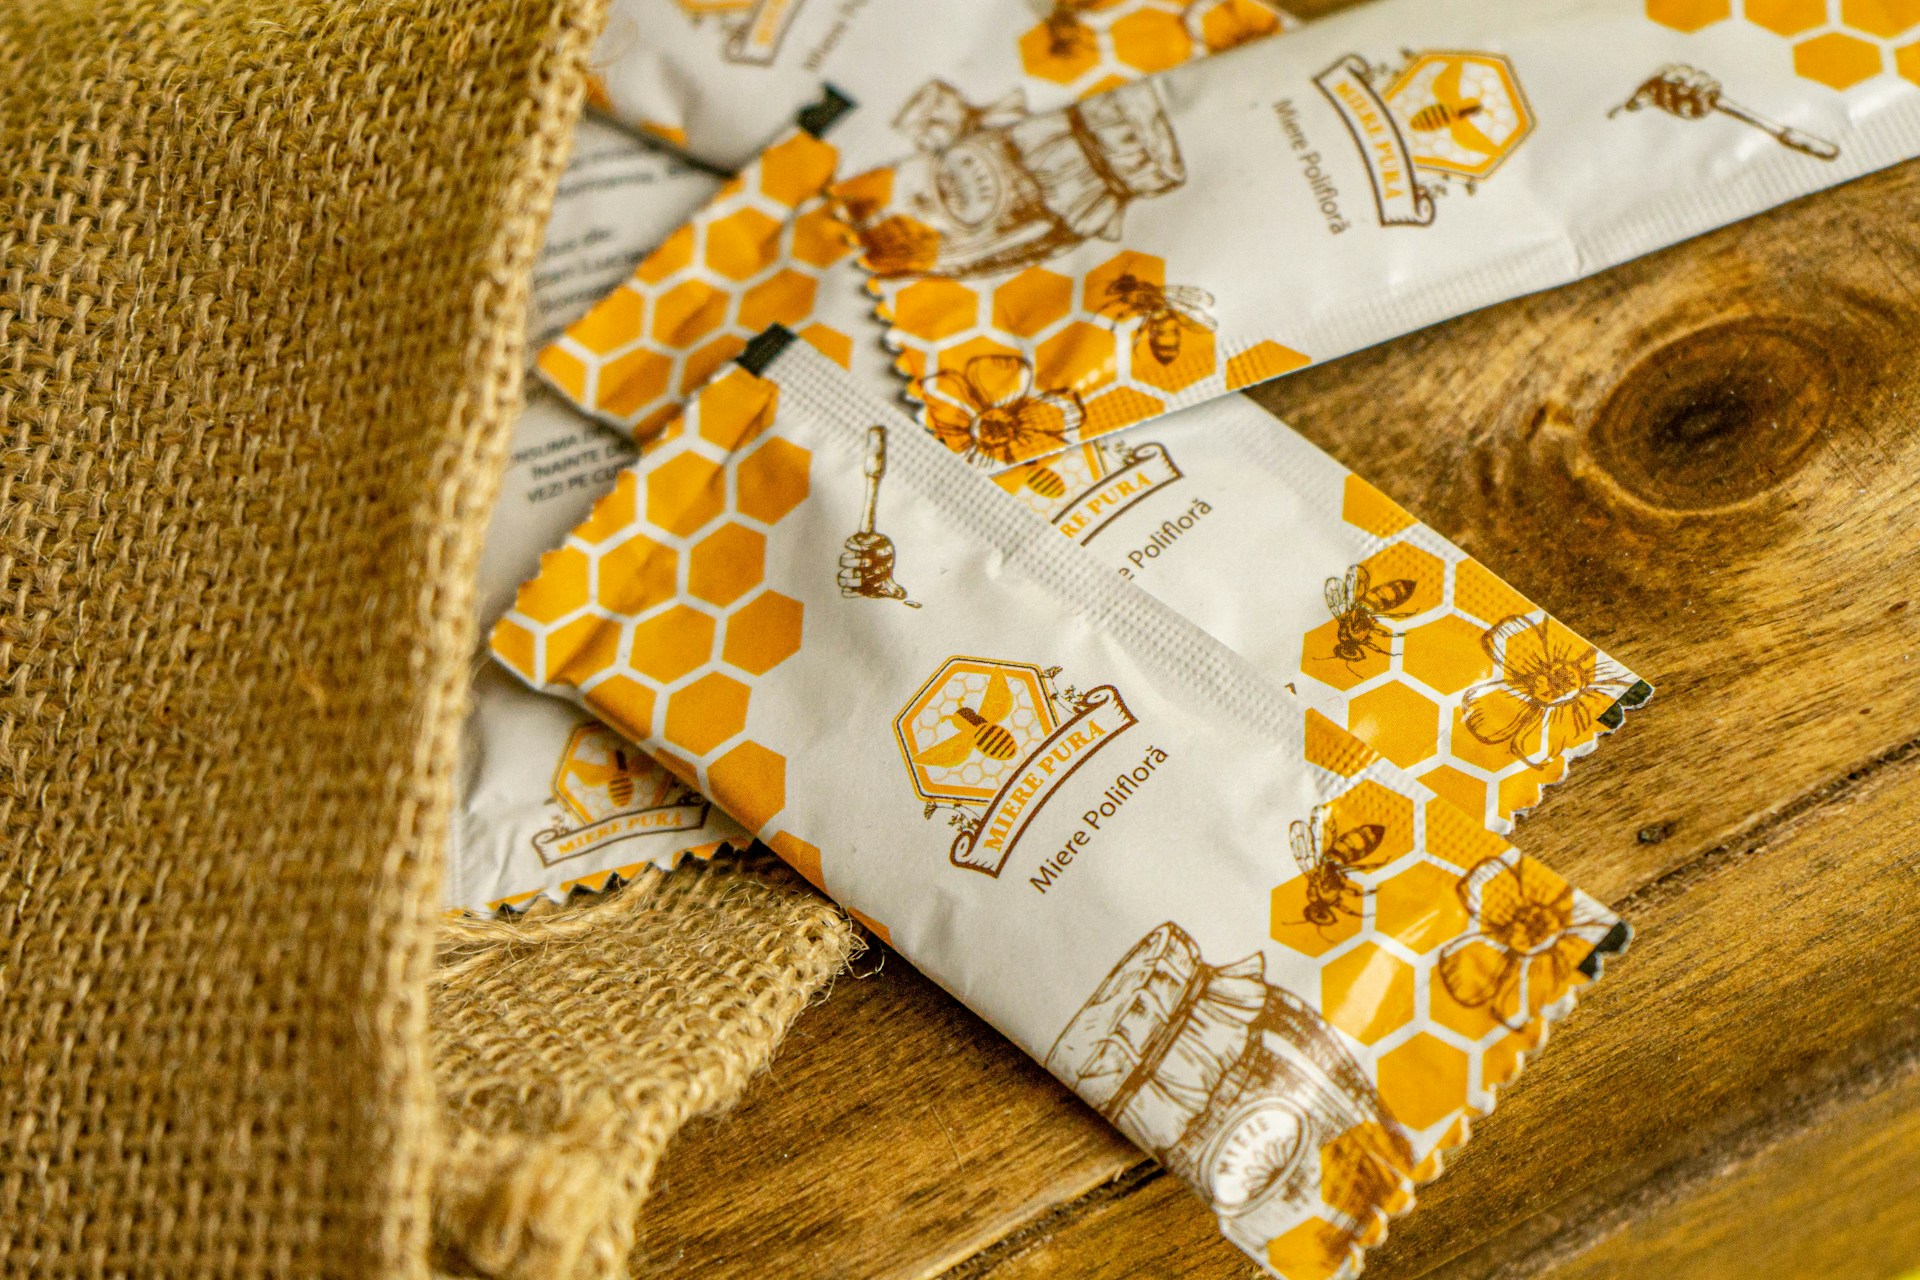
A stick pack is a narrow tube. A stick pack machine will take a single reel and split it into as many ribbons as the machine has lanes, with each ribbon drawn over a forming tube to shape it into a continuous sleeve, and a vertical seal closes the length of that sleeve. The doser drops a measured shot of product in, then a horizontal sealing bar closes the top of one stick and the bottom of the next before a blade separates them.
A sachet is flat. Two faces of film are drawn from a single reel, brought together and sealed down both edges to form an open-topped pocket in the sachet filling machine. The product is dosed in, the top sealed and a cutting station then separates the finished sachet from the web, giving a rectangular pack sealed on all four sides.This gives the sachet a continuous seal path, which matters most with three and four layer technical films where the seal quality decides whether the pack holds its stated shelf life.
You can explore all our single-dose packaging machine options in our sachet and stickpack machine range.
What each format holds well
Stick packs best suit single doses that pour, such as free-flowing powders, granules, liquids and semi-liquids – these all work well in a narrow tube, and the shape gives the customer an obvious way to use it: tear the top, tip it into a cup, a bottle or the mouth. The constraint is the tube itself. A larger dose has to be accommodated in length rather than width, and a stick that gets too long stops being convenient and starts being awkward to carton.
Meanwhile, sachets carry a wider spread of products, as the flat format has room across the width as well as the length. That makes it more forgiving for larger doses, and it handles pastes, capsules, tablets and single pieces that will not travel down a narrow forming tube cleanly.
Dosing is where the frame gets matched to the product, and the options are broadly the same on both formats. Product behaviour, rather than pack shape, usually drives that choice, and we cover it in more detail in our guide to filling liquids, powders and granules in flexible packaging.
It is worth knowing at specification stage: a single frame will not fill liquids and powders at the same time, because the dosing head is different for each. The machine can be built to accept interchangeable dosing systems where a line does need both.
Film is the running cost, not the capital cost
A stick carries one longitudinal seal and two cross seals. A sachet carries four. The seal area is film that holds no product, so for the same dose a stick typically uses around a third less film than a four-side-sealed sachet, though the exact difference moves with pack dimensions, dose volume and film structure.
A line running at high output gets through reel stock at a rate that can outweigh the capital cost of the machine within a few years, so film is the running cost that decides whether the format works commercially. It is also the most common source of seal problems, because film specified separately is more likely to have compatibility issues. We ensure the correct stick pack film and sachet film roll are supplied alongside the machine for that reason, matched to the product’s barrier and shelf-life requirements, including paper-based, aluminium-barrier and recyclable options where the application allows.
Output, lanes and pack size
The lane count is the main output lever on both formats, and it is directly tied to pack width, because every lane takes its own share of the same reel. Adding lanes raises throughput and narrows the pack at the same time.
More lanes also means more dosing heads to set, monitor and keep within tolerance. A twenty lane machine running slightly out on one lane produces a steady stream of underweight or overweight packs, so fill weight control gets harder as lane count rises, not easier. Where your target volume sits between two models, taking the larger frame with fewer lanes fitted usually leaves more room to grow.
Changeover is not one job
Recipe-level changes are quick on both formats. Fill weight, sealing temperature and pack length are settings stored per product and recalled from the touch screen, so a changeover between doses of the same pack width takes minutes.
Changing pack width is slightly different.. On stick packs it means changing the forming tubes and cutting arrangement; on sachets it means changing tooling. Both are physical changeovers rather than recipe changes, and the reel width has to suit the new format. The practical consequence is that every format the line is expected to run should be listed at specification stage, so the machine is built for the full set rather than adapted to it later.
Presentation, opening and secondary packaging
Pack width decides how much you can print. At 17mm to 140mm, a stick pack gives a narrow face with room for a brand, a flavour and the mandatory information, which is why sticks tend to be sold in outer cartons that do the selling. The pack itself is doing a convenience job.
A sachet runs from 40mm to 200mm wide and gives a flat panel on both faces, so it carries more branding, more on-pack information and easier space for multi-language copy. It also lies flat, which suits sampling, box inserts, on-pack attachment and display packs.
Finishing options are wider than most specifications assume. Both formats support laser scoring, rounded corners and diamond profiles; sticks add tear notches in vertical, inclined or V-shaped form, twin-pack configurations and child-resistant formats, while sachets add double and triplex multi-packs joined by perforation. Coding is integrated into the machine rather than added afterwards, with laser, inkjet and thermal transfer overprinting all running at line speed.
The two formats feed into secondary packaging differently, and this is a common late discovery. Sticks are usually counted and stood into cartons; sachets are often stacked or shingled. Whichever route you take, the end of line equipment needs to be specified against the pack you have chosen rather than adapted to it afterwards. It does not all have to be bought at once, as the machines are designed to integrate with secondary packaging equipment later without replacing what is already installed.
Confirming the format with your own product
Single-serve dosing is product-specific in a way that specification sheets cannot fully capture. Flow characteristics, temperature, moisture content and particle size all affect fill accuracy and seal quality, which is why we trial the product before quoting rather than working from the maximum figures. That trial is what turns a lane count and a pack width into a realistic sustained output. Installation and commissioning are carried out by our own engineers, with operator and maintenance training delivered on site at handover, and servicing, breakdown callouts and spare parts handled from the UK.
Speak to ILPRA UK about single-serve packaging
If you are weighing up stick packs against sachets, the quickest way through it is usually a conversation about the product, the dose and the output target rather than a comparison of pack shapes. Speak to our team about the format and machine configuration suited to your application.