Technology16 September 2026
Reducing downtime in automated food production lines
Line data usually tells the real downtime story: short stops, slow changeovers and idle machines quietly cut output every shift.
Major failures are disruptive, but they are also visible, investigated and acted on. The losses that quietly cap output on an industrial line are smaller, more frequent and rarely recorded in enough detail to be fixed. Reducing downtime usually means finding those losses first, then working on them through maintenance planning, better integration between machines and tighter control of changeovers.
The losses that do not look like downtime
Before maintenance strategy or new equipment comes into it, it helps to separate the different ways a line can lose time:
- Micro-stops. A tray misfeed, a film splice, a label reel change, or a reject flap that sticks. Each takes a minute or two and clears without an engineer, so it rarely gets logged at all.
- Reduced speed running. The line is moving, but below its rated rate, often to work around a fault nobody has had time to investigate properly.
- Changeover time. Tooling changes, cleaning between products, first-off checks and the settling period after a restart.
- Waiting. A machine starved by the process upstream or blocked by the process downstream. It is available, staffed and fault-free, and it is still not producing.
- Quality-related stops. Rework, re-running rejected packs, and holding output while a seal, weight or coding issue is confirmed.
Short stops and speed loss are the two that go missing most often. Unless they are recorded against reason codes, they show up only as an unexplained gap between what the line should produce in a shift and what it actually produces, which is very difficult to act on.
Measure before you fix
Overall equipment effectiveness (OEE) helps show where a production line is losing time. It breaks performance into three areas:
- whether the machine is available
- whether it is running at the right speed
- whether it is producing good-quality output
By recording planned maintenance, changeovers, breakdowns, short stops and speed loss separately, teams can see where the real problem is. Simple reason codes, used consistently every shift, are often more useful than very precise data that is only recorded occasionally. We cover how machine choice and line design shape output in our guide to how packaging machinery impacts production line throughput.
Maintenance planning and the parts that wear
Sealing tooling, jaws, gaskets, cutting blades, film feed components, drive belts, vacuum and pneumatic components all wear at a rate tied to cycles rather than weeks on a calendar. Schedules built around running hours or cycle counts tend to track reality better than fixed dates, particularly on lines where output varies seasonally. Service intervals and wear part lists should follow the machine’s current technical documentation rather than a general rule.
ILPRA UK covers technical service, spare parts and operator training through its service and maintenance support, including training for operators on correct machine use and production set-up.
Condition monitoring and predictive maintenance
Automated machines already generate most of the data needed to see a fault coming. Trending the metrics it provides over time shows drift before it becomes a stop, such as a sealing head creeping outside its normal temperature band, or an alarm that recurs slightly more often each week.
Predictive maintenance only reduces downtime where someone is responsible for that data and acts on what it shows. Our guide to packaging automation, machine controls and system integration goes into how these control systems work together.
Where lines lose time between machines
Individually reliable machines can still add up to a line that stops frequently, because lost time often occurs in the handovers between machines rather than in the machine itself:
- Buffering and accumulation. A sensible buffer between stages lets a short stop be absorbed instead of travelling up and down the line. Too little and every micro-stop causes an issue; too much and you are wasting product and floor space.
- Speed matching. Machines specified in isolation often run at rates that do not align, so one stage spends its day waiting on another. This is worth checking across the whole packaging machine line, not just at the stage that looks slowest.
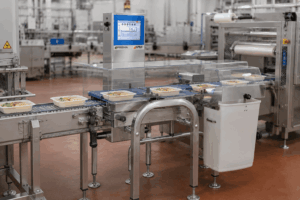
- Reject handling. Metal detectors and checkweighers only protect the line if rejected packs leave it cleanly. A jammed reject gate can easily stop production.
- End of line. Case packing, palletising and labelling are common places for a line to back up, particularly when pack format or case configuration changes.
Visibility across the line matters too. Understanding and monitoring potential sticking points across the whole line means that when a slowdown occurs, you can more easily identify and rectify the issue.
Material variation shows up as machine faults
Film gauge, sealing layer, tray tolerance and pouch quality all affect how consistently a machine runs. A film batch sitting at the edge of its tolerance can produce seal faults, misfeeds or breaks on equipment, which is why material problems are often misdiagnosed as machine problems. Keeping batch and supplier details alongside downtime records makes that pattern visible.
The same applies when moving to mono-material or recycled-content films. Seal parameters generally need re-establishing and trialling on the line rather than carrying across from the previous material, and compatibility depends on the machine, the tooling and the specific material specification.
Speak to us about increasing uptime on your line
If short stops, changeovers or recurring faults are limiting what your line produces, it is worth looking at the machinery. Speak to our team about the packaging machinery and configuration suited to your product, format and output targets.